Dairy
In dairy the pump is part of product quality. Shear determines body and texture, while dead volume determines microbiological safety.
The process
On the path from the fermentation tank to the filling line the product structure is at its most fragile. In set yoghurt and fresh cheese a gel structure, once broken, does not recover.
At the end of a run the same pump becomes part of the CIP circuit and operates through alkaline, acid and rinse phases at different temperatures and viscosities.
Fluid characteristics
- Thixotropic behaviour: viscosity drops under shear and only partly recovers at rest.
- High protein content tends to deposit on hot surfaces.
- CIP phases exceed 80 °C, and lines with SIP see direct steam contact.
- On low-viscosity media such as whey, slip flow determines efficiency.
Where it gets difficult
- High-speed pumps break the yoghurt gel and the product shows serum separation.
- Product retained around the shaft seal creates a microbiological risk that cleaning does not reach.
- Frequent temperature cycling shortens seal and elastomer life.
The Liquilob approach
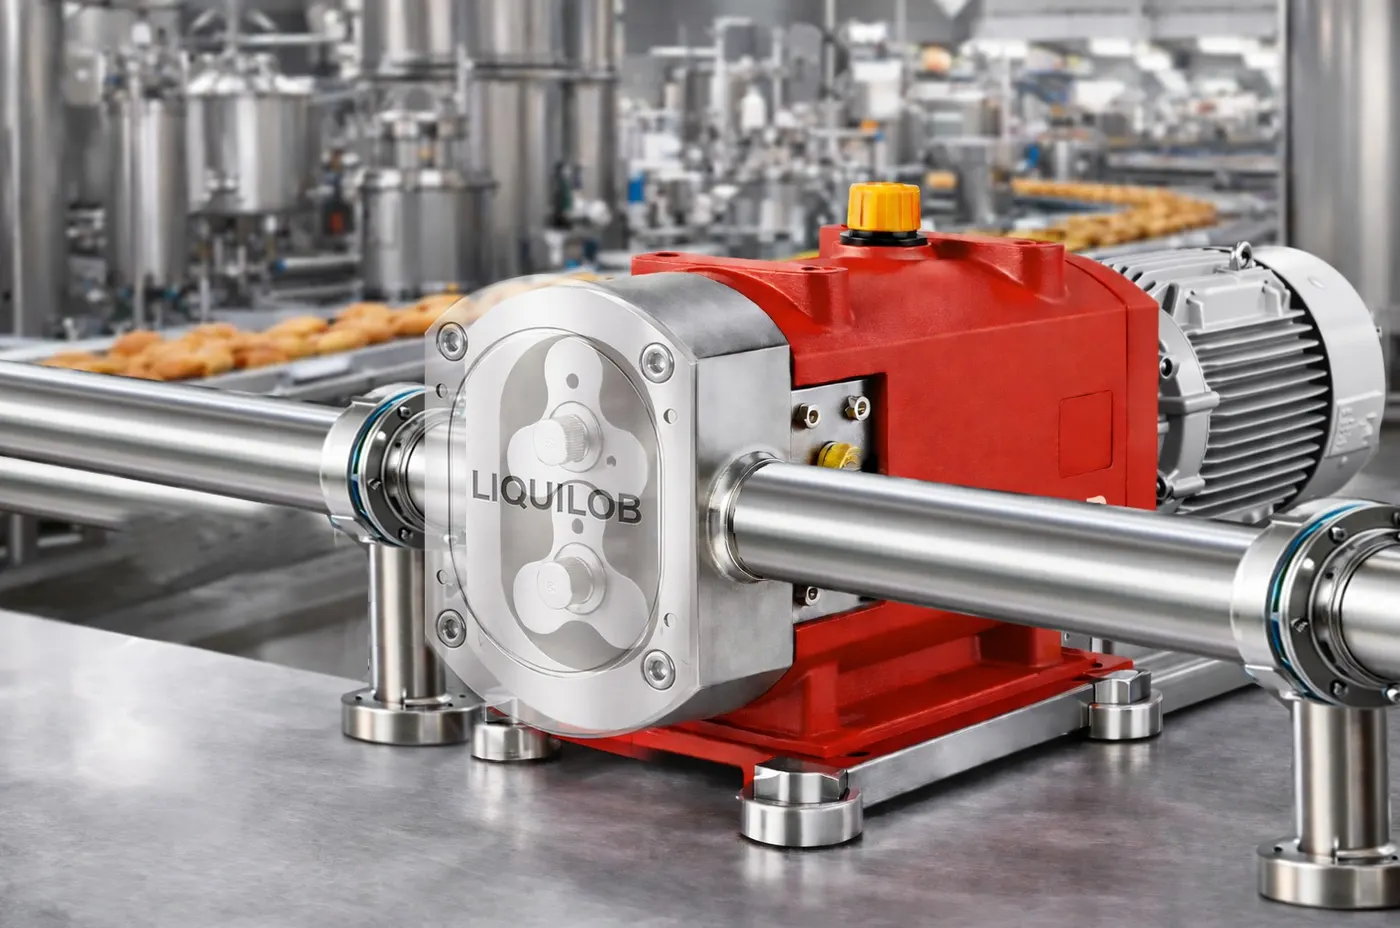
In the hygienic configuration the seal area is arranged so that CIP solution reaches it. With a flushed double mechanical seal the barrier fluid secures both sealing and cleanability.
For yoghurt and cream a bi-wing or tri-lobe rotor keeps shear low. Held near 200 rpm, the gel structure survives the transfer.
On lines with SIP the elastomer grade is specified as EPDM and the pump body is dimensioned for steam temperature.
Materials and hygiene
Let us determine the right pump for your application together.
Share your fluid characteristics and operating conditions, and our engineering team will help you arrive at the right Liquilob configuration.